Open Nav
When a pick-and-place machine drops a BGA component onto your board and the reflow oven produces a flawless array of solder joints, the outcome was determined long before the machine operator touched the line. It was determined during the design phase — when the land pattern was drawn, when the component spacing was set, and when the Dfm review either caught or missed the subtle incompatibilities between the design intent and the manufacturing process.
Component spacing and land pattern design are the most consequential — and most frequently neglected — aspects of SMT board design. Get them right and your assembly yields climb, your rework rates drop, and your Chinese manufacturer becomes a collaborative partner rather than a source of costly questions and delays. Get them wrong and no amount of process tuning in the factory will fully compensate.
This article covers the engineering principles, Ipc Standards, and practical manufacturing considerations that determine whether your board assembles flawlessly or fails repeatedly on the same defect classes — month after month.
The land pattern — the geometry of the copper pads onto which a Surface Mount component is placed — is not simply a replica of the component's lead dimensions. It is a manufactured artifact that must accommodate the realities of the assembly process: paste deposition, Component Placement, solder reflow, and thermal cycling. A pad that is the right size for the component datasheet may be the wrong size for the assembly process, resulting in tombstones, bridges, insufficient solder, or poor thermal joint integrity.
Similarly, component spacing — the distance between adjacent components and between components and the board edge — determines whether the pick-and-place machine can physically access each placement location, whether the reflow oven can heat components without causing thermal damage, and whether the Aoi system can inspect the completed assembly without occlusion.
In Chinese Contract Manufacturing facilities, the most common root cause of assembly defects — after paste printing — is design-related: land patterns that do not match the process capability, or spacing that violates the manufacturer's equipment constraints. These are problems that can only be solved in the design phase, not by adjusting machine parameters on the line.
The global PCB industry uses Ipc Standards as the common language for land pattern design, component spacing, and assembly acceptability. Understanding the relevant IPC documents — and how Chinese manufacturers interpret them — is the starting point for any discussion of spacing and land pattern optimization.
Ipc-7351 (Generic Requirements for Surface Mount Design and Land Pattern Standard) is the primary standard governing SMT land pattern geometry. It defines mathematical formulas for calculating pad dimensions based on component lead dimensions, tolerance stackup, and manufacturing process characteristics. The standard categorizes land patterns by density level — Nominal, Median, and Least — reflecting different levels of manufacturing tolerance accommodation:
Chinese manufacturers with modern equipment and good process control can reliably produce Median (M) density land patterns for most components. Less experienced manufacturers or facilities running at high utilization may require Nominal (N) patterns to achieve acceptable yields. When sending designs to a new Chinese manufacturer, using M-density patterns is a reasonable starting point, with adjustment based on actual yield feedback.
Ipc-a-610 (Acceptability of Electronic Assemblies) defines the visual and dimensional criteria for finished solder joints. It defines three acceptability levels — Class 1 (General Electronic Products), Class 2 (Dedicated Service Electronic Products), and Class 3 (High Performance Electronic Products) — with progressively stricter criteria at each level. For industrial and military applications, Class 3 is typically specified, imposing tighter requirements for fillet geometry, solder coverage, and defect thresholds.
Understanding Ipc-a-610 criteria matters for land pattern design because the acceptability limits define how much deviation from ideal joint geometry is acceptable. A land pattern that produces joints within Class 2 tolerances may be unacceptable for Class 3 applications, requiring redesign or tighter process control.
Chip components — 0201, 0402, 0603, 0805, 1206 and larger — are the most common SMT package types and the easiest to mis-design. The land pattern for a chip component consists of two rectangular pads with a gap between them. The pad length, width, and gap distance determine the solder joint geometry and thus the mechanical and thermal performance of the joint.
The Ipc-7351 formula for chip component land patterns calculates pad dimensions based on:
Common mistakes in chip land patterns include:
Quad Flat Package (QFP) and Small Outline Package (SOP) components have gull-wing leads on all four sides (for QFP) or two sides (for SOP). The land pattern must provide adequate solder wetting area for each lead while maintaining clearance between adjacent leads to prevent bridging.
Key land pattern parameters for QFP/SOP:
Ball Grid Array (BGA) and Chip Scale Package (CSP) components present the most demanding land pattern design challenges. The solder joints are hidden beneath the component body, making visual inspection impossible and making process control during printing and reflow absolutely critical.
BGA land pattern design parameters:
Quad Flat No-lead (QFN) and Small Outline No-lead (SON) packages have exposed pads on the bottom surface that serve as the primary thermal and electrical ground connection. The land pattern for the exposed pad is arguably the most critical feature of a QFN/SON design — a poorly designed thermal pad results in high thermal resistance, voids in the solder joint, and long-term reliability problems.
QFN thermal pad design guidelines:
The minimum spacing between adjacent components is determined by the constraints of the assembly and inspection processes, not just the component dimensions. A 0402 resistor placed 0.2mm from a neighboring 0402 might fit on the board, but it cannot be placed accurately by most standard pick-and-place machines, cannot be reliably inspected by Aoi, and cannot be reworked without disturbing the adjacent component.
General minimum spacing guidelines for Chinese Smt Assembly:
Components near the board edge are vulnerable to damage during depanelization — the process of separating individual boards from the manufacturing panel. Components placed too close to a V-groove or mouse-bite breakaway tab can be sheared off or have their solder joints cracked during depanelization.
Standard minimum distances:
Modern boards frequently stack multiple packages — a BGA under a QFP, or a passives array over a ground plane — creating a vertical density challenge. The tall component must not interfere with the shorter component during reflow or create shadows in the Aoi Inspection. Stacked package design requires careful review of the z-height envelope of all packages in the stack and verification that the reflow oven can heat both packages evenly without the taller package shading the shorter one from radiant heat.
Consistent component orientation — placing all resistors, capacitors, and ICs in the same direction relative to the reflow oven's airflow — significantly improves assembly yield. When a component is rotated 90 degrees in the placement program, the thermal profile it experiences during reflow may differ due to conveyor airflow asymmetry, creating uneven heating and increased tombstoning risk.
IPC-A-610 Class 3 requires all chip components on the same side of the board to have the same orientation — a requirement that is sometimes overlooked in designs with many small passives. Verifying orientation consistency during Dfm review prevents a Class 3 audit finding that could hold up an entire production lot.
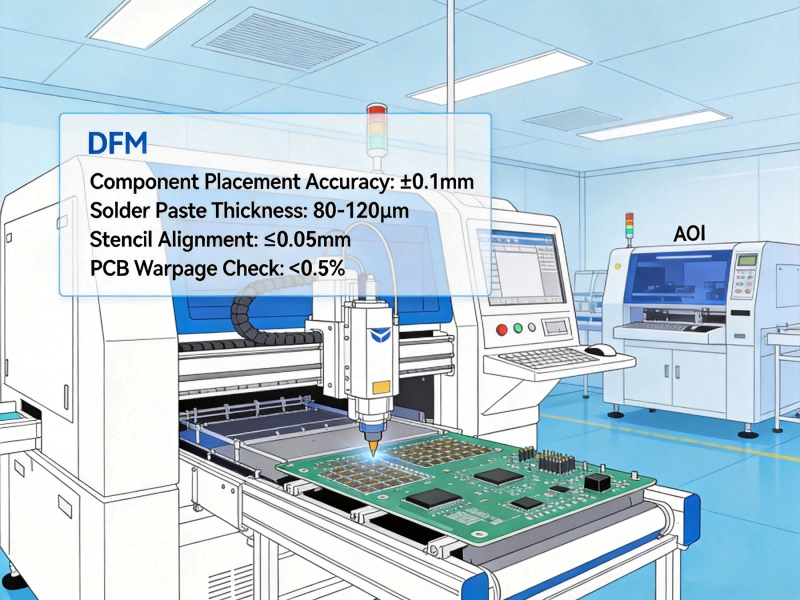
A quality-focused Chinese manufacturer conducts a Dfm Review — also called a design review or producibility review — before releasing a new design to production. The CAM engineering team examines the Gerber files, checks the land patterns against IPC-7351 guidelines, verifies spacing against their equipment constraints, and identifies any features that may cause assembly or test problems.
The output of a Dfm Review is a report listing identified issues, their severity, and recommended corrections. High-severity issues — those that will cause definite defects or production failures — must be corrected before production. Medium-severity issues — those that may cause defects under some conditions — are typically discussed with the customer for a risk-accept decision. Low-severity issues are noted but do not hold up production.
Common DFM findings related to land patterns and spacing:
The best way to ensure a smooth DFM and high first-pass yield is to follow IPC-7351 land pattern geometry for every component in the design, use the Median (M) density level unless your manufacturer specifically requests otherwise, and maintain a component spacing spreadsheet that documents the minimum distances between all adjacent component types.
Using a reputable EDA library — not hand-drawn land patterns — ensures that the patterns you use are based on the IPC-7351 formulas. Most major EDA tools include IPC-7351-compliant library parts as standard. When a component is not available in the standard library, generate the land pattern using the IPC-7351 calculator before hand-drawing it from scratch.
Finally, provide your manufacturer with a complete DFM checklist at the time of order: board dimensions, stackup, surface finish, and any special assembly notes. The more context you give the CAM team about the design intent, the better their review will be.
Fine-pitch QFPs with 0.4mm or 0.5mm lead spacing are among the most challenging packages to assemble reliably, particularly in high-mix, moderate-volume production environments. The narrow gap between adjacent leads — approximately 0.2mm for a 0.5mm pitch component — leaves very little margin for paste volume variation or placement offset.
For fine-pitch QFPs, the stencil design is as critical as the land pattern. Aperture reduction — typically 90–95% of the pad width — reduces paste volume to minimize bridging risk while maintaining adequate solder for a reliable joint. A laser-cut stainless steel stencil with electropolished walls is non-negotiable for 0.4mm pitch and finer. Nano-coating on the stencil surface further reduces paste adhesion to the walls and improves release.
Ultra-fine-pitch BGAs (0.4mm pitch and below) are increasingly common in modern electronics, particularly in processors, FPGAs, and high-density communication chips. At 0.4mm pitch, the ball diameter and pad diameter are both approximately 0.25mm, and the gap between adjacent pads is approximately 0.15mm — a dimension that demands precision manufacturing and tight process control.
For 0.4mm pitch and finer BGAs, NSMD pad definition is strongly preferred over SMD. The solder mask web between pads at 0.4mm pitch is too fragile to reliably maintain with SMD definition and is prone to cracking during thermal cycling, creating a solder bridge risk. NSMD eliminates this risk by defining the pad circumference through the pad opening itself rather than through the solder mask.
Not all Chinese SMT lines are created equal. High-volume facilities running 24/7 on mature products typically have equipment that is newer, better-maintained, and more tightly process-controlled than lower-volume or newer facilities. When sending fine-pitch designs to a new manufacturer, provide them with your IPC-7351 density level specification and ask them to confirm their equipment can achieve the tolerances required before committing to production.
The risk of not doing this: a manufacturer with older AOI equipment may not be able to inspect 0201 Components reliably, resulting in escapes. A facility with a older stencil printer may struggle with fine-pitch QFP paste deposition, causing bridges that require rework. These are solvable problems — but it is better to identify them during DFM review than after production starts.
Design intent that is obvious to the designer may not be obvious to a CAM engineer reviewing the files in a factory halfway around the world. Clearly label each layer in the Gerber file set, use standard file naming conventions, and include a readme file with any special assembly notes — for example, a note specifying that a specific QFN thermal pad requires void-free solder joints and the acceptable voiding percentage.
When a DFM report comes back with questions, respond promptly and specifically. The back-and-forth between the design team and the factory CAM team is where the best designs get even better and the mediocre designs are salvaged before they cause problems in production.
Land pattern design and component spacing are not the glamorous end of PCB engineering, but they are among the most consequential. A board with correctly designed land patterns — following IPC-7351 geometry, density level matched to the manufacturer's capability, spacing consistent with the assembly process — will assemble with minimal defects, inspect cleanly, and yield reliably at volume. A board designed without this rigor will produce a steady stream of defects: bridges, tombstones, insufficient joints, and buried failures that only manifest in the field.
The good news is that the standards and guidelines exist and are well-documented. IPC-7351 provides the formulas. IPC-A-610 provides the acceptance criteria. The DFM review process provides the forum for applying them to your specific design. Using these tools proactively — before you send your files to the factory — is the most effective cost reduction strategy available in Smt Assembly, because it eliminates the root cause of defects rather than managing the symptoms.
IPC-7351 is the industry standard for SMT land pattern geometry, providing mathematical formulas that calculate pad dimensions based on component lead dimensions, manufacturing tolerance stackup, and process characteristics. It defines three density levels — Nominal (maximum process margin), Median (balanced), and Least (maximum density) — allowing designers to choose the appropriate balance between board area efficiency and manufacturing ease. Using IPC-7351-compliant land patterns ensures consistency with what Chinese manufacturers' equipment and processes are designed to handle.
In Solder Mask Defined (SMD) pads, the solder mask opening is smaller than the copper pad, so the mask controls the solder joint geometry at the pad edge. In Non-Solder Mask Defined (NSMD) pads, the solder mask opening is slightly larger than the copper pad, so the copper pad circumference — not the mask — defines the solder joint boundary. NSMD is preferred for fine-pitch BGAs because the solder mask web between pads at 0.4mm pitch is too fragile to reliably protect against bridging and cracking under thermal cycling. NSMD gives better control over the solder joint geometry and reduces stress concentration at the pad edge.
A minimum clearance of 3.0mm between a BGA and the nearest adjacent component is recommended for standard assembly in most Chinese manufacturing facilities. This clearance is required for X-ray Inspection access, Bga Rework clearance, and to prevent thermal shading during reflow. For very fine-pitch BGAs (0.4mm and below), or when using manufacturers with more limited rework capability, increasing this to 5.0mm is advisable. Insufficient clearance between a BGA and adjacent components is one of the most common DFM findings and one of the easiest to prevent with early design attention.
Tombstoning (or drawbridging) occurs when a two-terminal surface mount component — typically a chip resistor or capacitor — lifts off one pad during reflow, leaving the other end soldered. It is caused by uneven heating of the two component terminations, which creates a differential in the surface tension of the liquid solder, pulling the component upright. Land pattern design prevents tombstoning by ensuring both pads are equal in size, thermal mass, and distance from the nearest thermal relief (such as thermal vias), so they heat at the same rate during reflow. Pad asymmetry — one pad significantly larger or better thermally connected than the other — is the primary land pattern cause of tombstoning.
For most industrial applications ordering from experienced Chinese manufacturers, IPC-7351 Median (M) density land patterns are the recommended default. M-density provides a balanced process window — tight enough to maximize board area utilization, loose enough to be reliably manufactured by most modern SMT lines. Least (L) density is suitable only for high-volume production with experienced manufacturers who have demonstrated first-pass yield at that density level. Nominal (N) density is appropriate for new product introduction, prototypes, or when qualifying a new manufacturer — it provides maximum process margin and is the most forgiving of process variation.
Before sending files, use the IPC-7351 calculator in your EDA tool to verify that all land patterns match the standard geometry for the specified component. Run a DFM check if your EDA tool supports it. Cross-check the minimum spacing between all adjacent component types against your manufacturer's capability data. For fine-pitch components (0.5mm pitch and finer), request confirmation from the manufacturer that their equipment can achieve the required placement accuracy and paste printing resolution. Finally, send a representative production sample to the manufacturer for pilot build before committing to high-volume production.
How to Reduce SMT PCB Assembly Costs in China with Early DFM AnalysisJune/17/2026
Essential DFM Guidelines for SMT PCB Assembly in ChinaJune/04/2026
Why DFM is Critical for High-Density BGA SMT Assembly in ChinaJuly/25/2026
The Role of SMT Assembly in China's Modern Industrial Automation and Robotics SectorAugust/08/2026
Optimizing PCB Design for Chinese SMT ManufacturersJuly/02/2026
Essential DFM Guidelines for SMT PCB Assembly in ChinaMay/29/2026
Understanding IPC Standards in DFM for SMT PCB Assembly China ProjectsSeptember/08/2026
Top 10 DFM Mistakes to Avoid Before Sending Files to China for SMT AssemblyJuly/14/2026